...

Cable Shielding Materials: Foil, Braid & EMI Design

Select foil, braid and hybrid shielding around frequency, grounding, motion, connector termination, cable size and production requirements.

Select foil, braid and hybrid shielding around frequency, grounding, motion, connector termination, cable size and production requirements.

  • Since 2012, SINO-CONN has supported custom cable assemblies from engineering through controlled production.
  • 1-piece prototype support for early fit, pinout and shielding validation.
  • Standard OEM production MOQ starts at 100 pcs, subject to material and connector conditions.

Cable Shielding Material Is Only Part of Performance

Cable shielding is not selected by metal name alone. Conductive material, shield geometry, coverage, termination, grounding, connector transition and cable routing work as one electrical and mechanical system.

Material, Construction and Shield Path Work Together

A shielding material is the conductive medium used around conductors or signal pairs. Copper, tinned copper, aluminum-laminated foil and metallized fabric are examples. Shield construction describes how the conductive material is arranged: foil wrap, braided shield, spiral serve, individual pair shield, overall shield or a combined structure.

The distinction matters during cable development. An aluminum/polyester foil can provide broad circumferential coverage with little increase in cable diameter, while a copper braid brings different mechanical behavior, termination options and current-carrying characteristics. Adding both layers can improve the shielding architecture for some applications, but also increases diameter, weight, assembly labor and termination complexity.

Shielding performance also continues beyond the cable body. A well-specified shield can lose much of its intended value when braid is poorly terminated, a long pigtail is used in a frequency-sensitive path, the connector shell is electrically discontinuous, or routing places a sensitive signal cable beside a strong switching-noise source.

SINO-CONN therefore treats shielding as a defined path from conductor or pair geometry through shield layers, drain or braid termination, connector interface and grounding strategy. Drawings can identify the relationship between Ground, Drain, Shield and Shell so the approved configuration is repeatable during prototyping and production.

Compare Cable Shielding Materials Before Freezing the BOM

Shield MaterialMain Engineering StrengthMechanical / Environmental ConsiderationTermination ConsiderationTypical Fit
Aluminum-Polyester FoilHigh circumferential coverage with low added ODFoil fatigue and overlap need attention in repeated motionCommonly paired with drain wire or defined foil terminationCompact signal cables, pair shields, overall shields
Bare CopperHigh conductivity and direct metallic pathWeight, oxidation exposure and braid geometry matterSupports braid, serve and direct metallic termination methodsIndustrial, signal and grounding-oriented constructions
Tinned CopperConductive copper base with improved surface oxidation resistanceAdds braid thickness and weight; flex depends on braid designWell suited to crimp, clamp, backshell or grounding structuresIndustrial harnesses, shielded assemblies, grounding sleeves
Silver-Plated CopperUsed for specialized high-frequency or temperature-driven designsHigher material cost and project-specific compatibility reviewRequires controlled connector and shield terminationRF, aerospace-style or specialized interconnect designs
Conductive FabricLightweight and conformable around irregular geometryAbrasion and retention require evaluationGrounding method must be deliberately designedBranch transitions, localized wraps, flexible shielding
Specialty Metal / MeshCan address unusual temperature, corrosion or mechanical requirementsOften changes stiffness, weight and bend behaviorTermination may require dedicated hardware or processHarsh or project-specific environments

Foil vs Braid vs Foil Plus Braid

No single shield construction wins every comparison. Start with signal and interference conditions, then account for motion, cable diameter, connector termination and production cost.

Decision FactorFoil ShieldBraid ShieldFoil + Braid
Physical CoverageBroad circumferential coverage when wrapped correctlyDepends on braid geometry and coverage specificationCombines foil coverage with braided outer path
Cable DiameterLow added thicknessAdds more OD than foil in many constructionsUsually the largest of the three
Cable WeightLowHigher due to metallic braidHighest when both layers are used
Repeated FlexRequires careful construction reviewCan suit flexible designs when braid and cable are engineered for motionMust evaluate interaction of both shield layers
Mechanical ProtectionLimitedBraid adds useful mechanical reinforcementHigher structural complexity
TerminationOften uses drain wire or defined foil contactCan be clamped, crimped or terminated to shell/backshellRequires deliberate control of both layers
Manufacturing CostUsually lower material and labor burdenMore braid material and termination workHigher material and assembly complexity
Best Starting PointCompact static or moderate-motion signal designsRobust shield path and mechanically demanding applicationsHigher-noise or broader shielding requirements where OD allows

What Actually Determines Cable Shielding Effectiveness

Material conductivity matters, but strong shielding depends on the complete electrical path. Coverage, frequency, connector geometry, grounding and routing can outweigh a simple material upgrade.

Build One Continuous Shielding System

Shielding should be reviewed from the interference source to the sensitive circuit and from the cable core to the equipment ground or chassis. Material is only one variable.

  • Coverage and openings: A foil wrap, braid or mesh has a physical geometry. Gaps, braid openings, branch breakouts and poorly overlapped sections can create different behavior at different frequencies. Coverage should therefore be specified from an actual cable design rather than copied as a generic marketing number.
  • Termination: A shield has little value if its electrical path ends abruptly before the connector. Drain wires, pigtails, braid clamps, conductive backshells and 360-degree shell termination solve different packaging and electrical problems. Longer exposed shield-to-shell paths can become increasingly important as frequency rises.
  • Grounding: Signal return, power return, protective earth and chassis ground should not be treated as one undefined “GND.” The grounding arrangement should follow the equipment architecture, not a universal rule about connecting one end or both ends.
  • Connector transition: Shield continuity can change where a cable enters an overmold, backshell or plastic connector body. Metallic shell contact, shield fold-back, braid length and strain-relief geometry belong in the controlled assembly definition.
  • Routing: A well-designed shield cannot compensate for every installation problem. Parallel routing beside motor, VFD or switching-power conductors, poor separation, ground discontinuities and sensitive pair geometry may still create EMI or signal-integrity issues.

SINO-CONN can translate these inputs into drawings, shield-to-ground maps, termination details and prototype validation requirements before production release.

Match Shielding to Frequency and Noise Conditions

A shield should be selected around the actual interference mechanism. Motor noise, high-speed differential data, RF transmission and mixed power-signal harnesses require different engineering priorities.

High-Frequency Interference

Higher-frequency interference makes shield continuity and termination geometry increasingly important. Short shield-to-shell paths, controlled connector transitions and appropriate cable construction deserve more attention than simply adding more metal. For RF or high-speed designs, signal frequency, cable length, connector type, grounding arrangement and required insertion-loss, return-loss, impedance or functional criteria should be defined before release. A generic shielding material cannot establish these performance limits without the complete construction and test conditions.

Motor And VFD Noise

Motor drives, inverters and switching power equipment can create strong common-mode and radiated noise around nearby signal cables. Shield material is only part of the solution. Routing separation, chassis connection, connector shell treatment and the relationship between power and sensitive circuits can determine whether interference reaches the receiving electronics. Industrial cable development should therefore begin with equipment type, cable route, motor/VFD location, grounding diagram and signal function before choosing foil, braid or a combined shield.

High-Speed Differential Signals

LVDS, eDP, MIPI, Ethernet, USB and other differential links depend on pair geometry, impedance, return path, connector transition and shielding working together. A cable can pass continuity testing and still fail at operating speed when pair spacing, untwist length, termination or shield continuity changes. SINO-CONN reviews protocol or frequency, length, connector P/N, pair definition and installation constraints together, then applies TDR, RF or functional validation where required by the project.

Mixed Power And Signal

Hybrid assemblies containing power conductors, low-level analog circuits, control signals and high-speed data may need selective shielding instead of one heavy overall layer. Individual pair shielding, physical separation, grounded foil or braid and overall shielding can be combined according to coupling risk. The design must also account for branch points, connector pin assignment, cable OD, heat, installation space and termination access. A shield architecture should reduce interference without turning the harness into an unnecessarily large or rigid assembly.

Shield Termination and Grounding Need Equal Attention

A premium shielding material can underperform when the end connection is poorly controlled. Define the shield path at every connector, branch, drain and chassis connection.

Drain Wire And Pigtail

Drain wires provide an accessible electrical connection to foil or other shield structures, but their length, routing and termination must be defined. A long pigtail can introduce unwanted impedance in frequency-sensitive applications, while an uncontrolled drain wire can create inconsistent assembly results. Drawings should identify drain wire gauge where relevant, exposed length, termination point and relationship to shell or ground. Production should not decide these details from appearance or previous jobs.

360-Degree Termination

A 360-degree termination connects the shield around the cable circumference to a conductive connector shell, clamp or backshell. It can reduce the unshielded transition created by a long pigtail and is often considered for frequency-sensitive industrial, high-speed or RF applications. The mechanical design must still provide reliable compression or retention without damaging the cable. Backshell size, braid fold-back, jacket strip length, strain relief and mating hardware all need to fit the connector and installation envelope.

Grounding Strategy

Single-end grounding and double-end grounding are engineering choices, not universal rules. Frequency, chassis architecture, ground-loop risk, equipment grounding and noise mechanism influence the correct arrangement. SINO-CONN follows the system grounding requirement supplied by the project and converts it into a cable-level Shield-to-Ground Map. Signal return, power return and chassis/protective ground can be identified separately so a production drawing does not reduce every connection to an ambiguous “GND.”

Branch And Connector Transition

Multi-branch harnesses often lose shielding consistency where an overall shield divides into several legs. The branch needs a defined treatment: continued individual shields, conductive wrap, local braid, ground splice, shell connection or an intentionally unshielded section. Connector exits create another transition where overmold, heat shrink and strain relief may interfere with shield access. A controlled drawing should define shield cutback, overlap, branch continuity and termination before prototypes are built.

Balance Shielding With Flexibility, Bend and Cable Size

More shielding can improve one requirement while hurting another. Cable OD, stiffness, bend radius, motion and connector exit geometry should be checked before adding layers.

Static Installations

Fixed equipment can often tolerate a more robust shield stack because repeated cable flexing is limited after installation. Foil, braid or combined structures can be selected mainly around EMI conditions, available space, grounding and mechanical protection. Static does not mean unrestricted: bend radius at installation, connector exit angle, panel openings and bundle compression still matter. Overbuilding the shield can increase OD and assembly difficulty without adding useful performance if the actual interference environment is modest.

Repeated Flexing

A cable used in repeated bending experiences movement across conductors, insulation, foil, braid and jacket at the same time. A construction selected only for static EMI performance may become a fatigue point during motion. Foil can be vulnerable in unsuitable repetitive-flex structures, while braid geometry and jacket selection also influence flexibility. Bend radius, bend direction, cycle rate, moving length and load should be defined before selecting a dynamic shield construction rather than attaching a generic flex-life claim.

Torsion And Robotics

Robot joints, rotating heads and articulated equipment can introduce torsion in addition to bending. Shield strands, pairs and conductors must accommodate repeated angular movement without uncontrolled migration or concentration of stress near connectors. Shielding should be evaluated together with conductor stranding, cable lay, jacket, branch geometry and strain relief. A torsion requirement therefore needs actual motion angle, moving zone, routing, cable length and fixture conditions rather than a single statement such as “high-flex shielded cable.”

Tight Installation Space

Foil offers useful coverage with limited added thickness, while braid, sleeving, overmold and backshell hardware can quickly increase the local envelope. Reducing OD by removing a shield layer, however, can create EMI or mechanical compromises. Engineering review should start with maximum cable OD, pass-through size, connector envelope, minimum bend zone and routing path. SINO-CONN can use 2D/3D information to evaluate fit when a compact assembly has competing electrical and mechanical requirements. 

Information Needed for a Shielding Engineering Review

Engineering InputWhat To ProvideWhy It Matters
Signal / ProtocolAnalog, LVDS, MIPI, Ethernet, USB, RF, encoder, sensor, control, etc.Defines signal sensitivity and shielding priorities
Frequency / Data RequirementOperating frequency, data rate or interface specification where applicableHelps determine transition, return-path and validation needs
ConnectorManufacturer P/N, series, photo or mating interfaceDetermines shell, pinout and termination possibilities
Pinout / Circuit MapPin-to-pin definition, pair grouping, ground and shield pinsPrevents shield and return-path ambiguity
Cable LengthOverall and branch lengths with toleranceInfluences routing, loss, voltage drop and assembly control
Current ShieldExisting foil, braid, drain wire or cable P/N if replacing a designEstablishes the starting construction
GroundingChassis, shell, drain, single-end/double-end or existing schematicDefines the shield termination path
MotionStatic, occasional bend, repeated flex, torsion, drag-chainInfluences foil, braid, conductor and jacket selection
EnvironmentTemperature, oil, chemical, UV, water, vibration or abrasionDrives material and protection requirements
Installation SpaceMax OD, pass-through, bend zone, connector envelopePrevents shielding from creating fit problems
Existing ProblemEMI symptom, signal drop, unstable link, EMC report or photosHelps narrow probable causes
ValidationContinuity, functional, RF/SI, flex, environmental or report requirementDefines prototype and production verification
QuantityPrototype, trial batch and expected production volumeSupports material sourcing, tooling and commercial planning

Complete drawings are helpful but not mandatory at the first contact. Send the information already available; missing fields can be clarified before a prototype construction is released.

Prototype Shielding Before Releasing Production

A shielding concept should be converted into an approved physical assembly before scale-up. SINO-CONN supports development from incomplete requirements through drawing, sample and validation.

Requirement Review

Development can begin from a drawing, BOM, connector P/N, sample, photo or functional requirement. The first review identifies signal type, connector interface, shield structure, grounding, cable length, motion, environment and testing needs. Unknown information is converted into engineering questions rather than guessed into production. For replacement projects, an existing cable can also be used to identify shield layers, drain routing and termination details.

Construction Proposal

Engineering translates the requirements into a proposed cable stack and termination method. Foil, braid, drain wire, individual pair shielding, overall shielding, jacket and connector-end treatment are considered together. Alternative constructions can be compared when OD, flexibility, supply risk or cost creates a conflict. Proposed changes remain subject to project approval before they become the manufacturing baseline.

Drawing And BOM

The selected structure is recorded in controlled documentation. Drawings can identify pinout, pair grouping, shield-to-ground relationships, strip lengths, branch dimensions and connector orientation. The BOM identifies cable, connector, terminal, shield materials, heat shrink, backshell and other controlled items. Approved alternatives are separated from original specified materials rather than silently substituted.

Prototype Build

SINO-CONN supports one-piece prototyping for early validation. Standard or in-stock samples are typically prepared in 2–3 working days, while custom-developed samples are typically 5–10 working days depending on complexity, component availability and engineering requirements. Prototype work is used to verify fit, pinout, electrical function, materials and manufacturability before scale-up.

Shielding Validation

Prototype checks follow project risk. Basic work can include pin mapping, continuity, shield continuity, dimensions and connector mating. High-speed, RF, repeated-motion or EMI-sensitive projects may require additional functional, TDR, VNA, flex or equipment-level evaluation. The acceptance method should be defined before interpreting results; one passing continuity test is not evidence of RF, high-speed or EMC performance.

Revision Freeze

Feedback from the prototype is written back into the drawing, BOM, process instructions or test criteria. Once the approved configuration is stable, the project can move into pilot or production using the confirmed revision. Connector, shielding material, grounding and termination changes should not be introduced on the production floor without controlled review and approval.

Control Shielding Details During Cable Assembly Production

Shielding quality is built at cutting, wrapping, braiding and termination stages. Process control focuses on the details that can change electrical continuity, cable geometry and repeatability.

Foil, Drain Wire and Braid Processing Control

Shield preparation starts before the connector is installed. The operator must know which shield belongs to each circuit, how far it is stripped, whether foil must remain intact through a transition, and where braid or drain wire will terminate.

Foil preparation: Strip length and foil cutback need to match the released drawing. Excessive removal can enlarge the unshielded section; careless stripping can nick insulation, disturb a twisted pair or damage the foil layer. Where overlap or local conductive wrap is specified, the direction and coverage zone should remain consistent with the approved construction.

Drain-wire control: Drain wires require clear identification and a controlled termination point. Length, routing and insulation treatment should prevent accidental contact with unrelated circuits. For multi-shield assemblies, production documentation should make it impossible to confuse one pair’s drain with another.

Braid handling: Metallic braid can spread, fray or lose coverage when it is pushed back or cut. The work instruction should define preparation length, fold-back direction, retention and termination method. A braid used for shielding must not be confused with PET expandable sleeving used only for mechanical protection. SINO-CONN’s internal material logic separates external protective braid from conductive shielding braid.

Geometry protection: High-speed and coaxial assemblies also require control of pair untwist, exposed conductor length and shield transition close to the connector. A shield process that passes visual inspection but disturbs controlled signal geometry can still create functional problems.

The objective is not simply to “add a shield.” Production must reproduce the same defined shield path on every approved assembly.

Validate Shielding With the Right Test Method

Inspection should match the risk being controlled. Basic electrical checks, mechanical verification and high-frequency testing serve different purposes and should not be presented as interchangeable evidence.

Electrical Baseline

Production assemblies are controlled against the approved drawing and test plan, with SINO-CONN’s published manufacturing system using 100% full inspection as the baseline. For shielded assemblies, electrical checks may include pin-to-pin continuity, open/short detection, shield continuity and defined shell or ground connections. A continuity result proves the intended conductive path exists; it does not prove EMI attenuation, impedance or high-speed link performance.

Mechanical Verification

Shielding can fail mechanically before an obvious electrical fault appears. Pull, bend, flex, connector retention, dimensional inspection and visual checks are selected according to the assembly and application. Dynamic tests require defined bend radius, angle, cycle rate, load and failure criteria rather than a standalone cycle number. Connector exits, braid cutbacks and rigid transition areas deserve special attention because stress often concentrates near the termination.

Signal And RF Validation

High-speed digital and RF assemblies may require TDR, impedance, functional communication, insertion loss, return loss or VSWR evaluation according to the interface and project specification. Test values must be tied to cable type, connector configuration, length, fixture and frequency range. SINO-CONN does not treat a normal resistance or continuity test as proof of signal integrity when the application depends on controlled transmission characteristics.

EMI And System Boundary

Cable-level testing can verify shield continuity, termination, construction and selected electrical characteristics. Final equipment EMC performance also depends on enclosure design, PCB return paths, chassis bonding, power architecture, filtering, grounding and installed routing. A shielded cable should therefore never be presented as an automatic guarantee that an assembled machine will pass a particular EMC standard. Equipment-level compliance remains subject to the applicable system test.

Shielding Development Case for an Industrial Imaging Cable

An anonymized 1,200-piece production program shows how shield selection becomes a controlled cable assembly rather than a material-only purchasing decision.

From EMI Concern to a Repeatable 1,200-Piece Build

An industrial imaging program required a shielded cable assembly for a camera connection installed near switching and motor-control wiring. The production order was set at 1,200 pcs, reflecting the volume range commonly handled in established brand programs rather than a one-off laboratory cable.

The initial discussion focused on whether more braid should be added. Engineering review shifted the decision toward the complete shield path: signal grouping, existing foil structure, grounding relationship, cable routing, connector transition and available installation space. Increasing shielding thickness without checking the connector end would have increased OD while leaving the most sensitive transition unchanged.

The proposed production definition therefore separated the work into four controlled decisions:

  • Cable structure: preserve the required signal geometry and use an approved shield construction rather than adding an undefined outer layer.
  • Termination: define drain/braid handling and the connection to the intended ground or shell directly in the drawing.
  • Mechanical transition: control strip length, shield cutback and strain relief so connector-end processing would not disturb the shielding geometry.
  • Validation: check mapping and shield continuity as production controls, with application-specific functional evaluation before final production release.

After the configuration was approved, material identity, termination details and critical dimensions were frozen in the BOM and drawing. Production followed the approved revision rather than allowing operators to adjust shield length or grounding by experience.

The value of the work was not a claim that one shielding material solved EMI. The program converted an interference concern into a repeatable cable construction with defined materials, connections, manufacturing steps and verification points—exactly what a 1,200-piece repeat order needs.

Shielding Design Affects Cost, MOQ and Lead Time

Commercial terms come from the actual construction. Material layers, connector hardware, termination labor, testing and sourcing can change feasibility more than cable length alone.

Cost Drivers

Shielding cost includes more than the raw foil or braid. Braid material, coverage specification, individual pair shields, double shielding, drain wires, backshells, conductive hardware, extra stripping operations, branch treatment and inspection all add cost. A heavy foil-plus-braid structure may be unnecessary for a moderate-noise application. SINO-CONN can compare constructions around required performance, cable OD, manufacturing effort and material availability before the BOM is frozen.

MOQ Drivers

SINO-CONN’s standard OEM production MOQ uses 100 pcs as the baseline, while prototype work can start from one piece. Actual production feasibility still depends on connector pack quantity, special cable MOQ, braid or foil procurement, tooling, test fixtures, SKU mix and required compliance documentation. Higher-volume brand programs are normally evaluated against forecast, material supply and repeat-order requirements rather than forcing every shielding design into the same quantity rule.

Lead-Time Drivers

For standard products or smaller production orders, the published typical lead time is 5–7 working days. Large or fully customized orders are typically 10–25 working days, including procurement, assembly, testing and final packaging. Shielding can extend the critical path when special cable construction, customer-specified material, backshell hardware, tooling or added validation is required. Final timing should therefore be confirmed after the connector, cable construction, quantity and test requirements are known.

Build Compliance Into the Shielding Material BOM

Compliance should be attached to the exact cable, component, material and revision. A generic certificate list cannot prove that every shielding construction meets every market requirement.

RoHS And REACH

Shielding materials and related components can be selected and documented for project-specific RoHS and REACH requirements. The approved BOM should identify the exact cable, braid, foil, heat shrink, connector and other controlled materials involved. Supplier declarations or test documentation should correspond to the relevant material or component rather than being applied broadly to unrelated assemblies. A material substitution can therefore trigger a compliance review even when electrical dimensions appear unchanged.

Wire And Material Ratings

Projects calling for a particular flame, temperature, halogen, cable or recognized-component requirement need the exact approved grade to support the claim. “PVC,” “copper braid” or “foil shield” alone is not an adequate compliance specification. Material grade, supplier P/N, applicable recognition or test evidence and drawing revision should remain connected. SINO-CONN’s knowledge rules explicitly require material ratings to follow the exact grade and applicable test conditions.

Assembly Standards

IPC/WHMA-A-620 can be used as an assembly acceptance reference where required by the contract, drawing or project quality plan, with acceptance class and applicable revision defined for the program. It should not be presented as a blanket certification of every cable assembly. Customer drawings, specifications and approved inspection criteria take precedence where they establish more specific requirements.

Traceable Documentation

Depending on project requirements, the documentation package can include approved drawing and BOM revisions, material declarations, inspection records, test reports, FAI information, COC or other agreed quality records. A COC is a manufacturer declaration tied to an order, part number and revision; it is not the same as a third-party certificate. Strong compliance control keeps the evidence attached to the assembly actually supplied instead of relying on a general website claim.
Cable Shielding Materials Frequently Asked Questions
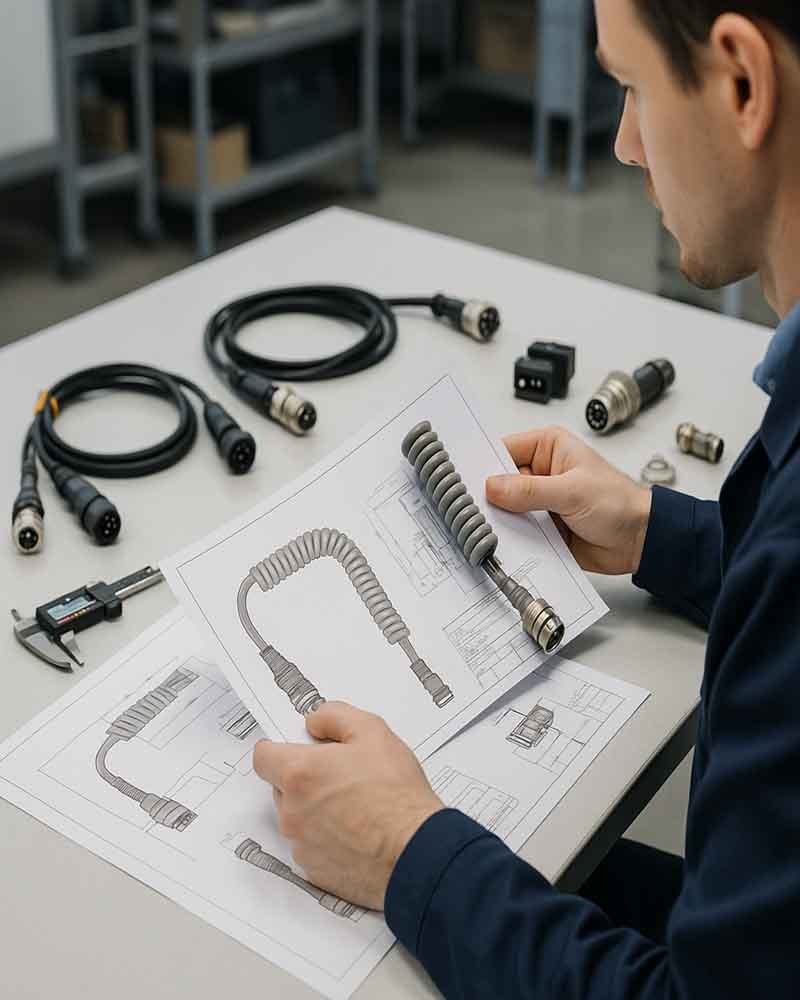
There is no universal best material. Aluminum foil, copper braid, tinned copper braid and other conductive materials solve different combinations of EMI, flexibility, weight, diameter, corrosion, termination and cost requirements. Start with signal type or frequency, interference source, grounding, cable motion, connector design and installation space. The final choice should then be fixed to an exact cable or material specification.
Not in every application. Braid can provide a robust metallic path and useful mechanical behavior, while foil can provide broad coverage with lower added diameter and weight. Dynamic movement, frequency, termination, cable size and cost can change the preferred construction. Foil plus braid is also available where the project justifies both layers.
Tinned copper retains the conductive copper base while providing a tin-coated surface that can improve resistance to surface oxidation and support common termination processes. It is widely used in shielded cable and grounding constructions. Actual braid coverage, strand design, temperature capability, flex behavior and termination method still depend on the specific approved cable or braid specification.
Foil can be used in flexible cable designs, but repeated-motion applications need careful construction review. Foil type, overlap, supporting layers, conductor design, jacket and bend conditions all influence durability. For robotic or continuous-flex applications, define bend radius, motion direction, torsion, cycle rate and installation conditions before selecting the shield instead of assuming every foil cable has the same flex life.
Braid coverage describes how much of the underlying cable surface is physically covered by the woven metallic strands. It depends on strand size, carrier count and braid geometry. A higher percentage is not automatically the complete answer to EMI performance because frequency, termination, grounding, connector transition and routing also matter. Use the actual cable specification rather than assuming a universal coverage value.
No. Drain wires are commonly used with foil and some combined shield structures because they provide an accessible connection to the shield. Other designs may terminate braid directly to a shell, backshell, clamp or ground hardware. The correct method depends on cable construction, connector system, grounding architecture, frequency and manufacturing requirements.
Neither method is universally correct. Grounding depends on frequency, equipment architecture, chassis bonding, ground-loop risk and the intended shield function. Signal ground, power return and chassis ground should also be distinguished. Supply the grounding schematic or system requirement so the cable-level termination can be defined in the drawing.
Usually, additional shield layers increase material around the cable core. Braid can add diameter and weight, while foil generally adds less thickness. Foil-plus-braid, external sleeve, overmold and backshell hardware can increase the local envelope further. OD reduction should not sacrifice EMI, flex, mechanical or electrical requirements, so installation space should be reviewed with the complete construction.
Yes. Foil-plus-braid constructions are common where a project benefits from complementary shield structures. The combination also adds cost, weight, diameter and termination work, so it should be selected for a defined reason. The connector end must preserve the intended relationship between foil, braid, drain, shell and ground.
Send whatever is already available: connector P/N or photos, pinout, signal/protocol, frequency or data requirement, cable length, current shield construction, grounding, motion, environment, installation space, drawings, sample photos and quantity. An existing cable or failed sample can also start the review. Missing specifications can be clarified before prototype release.

Send Your Shielding Requirements for Engineering Review

A useful quotation starts with enough information to identify the cable architecture, not a perfectly finished specification. SINO-CONN can begin from a drawing, BOM, connector P/N, pinout, existing sample, equipment photo or functional requirement and convert the available information into a manufacturable shielding definition. For the fastest review, include:
  • Signal type, protocol, frequency or operating function
  • Connector manufacturer P/N, mating interface or clear photos
  • Pinout and any shield, drain, shell or ground assignments
  • Overall length, branch lengths and dimensional tolerances
  • Existing foil, braid, drain wire or cable specification
  • Static, repeated-flex, torsion or drag-chain conditions
  • Maximum cable OD, routing path and available bend space
  • Temperature, oil, water, chemical, vibration or abrasion conditions
  • EMI symptoms, EMC information or current cable problems where relevant
  • Required inspection, functional, RF/SI or mechanical validation
  • Prototype quantity, production quantity and expected repeat demand
  • Drawing, BOM, photo, sample or existing cable P/N
Sensitive drawings and technical files can be reviewed under the appropriate project confidentiality process. Engineering then clarifies missing inputs, defines the cable and shield construction, confirms the prototype path and establishes the production quotation against the approved requirements.

Ask For A Quick Quote

We will contact you within 24 Hours, please pay attentionto the email with the suffx”@sino-conn.com”.